View:43432Time:2026.09.24
A glossy digital rendering will make almost any custom medal manufacturer's work look impressive — which is exactly the problem. Rendered mockups can't show you how heavy a medal actually feels in the hand, whether the plating will hold up after a few months of handling, or whether the enamel color truly matches your event's branding rather than an approximate shade. Real quality differences between suppliers only become visible when you know specifically what to look for in a physical sample, and most first-time buyers simply don't know what questions to ask or what details to inspect. This guide walks through exactly how to evaluate custom medal manufacturer quality across five concrete dimensions — metal weight and density, electroplating and surface polish, enamel color accuracy, ribbon and assembly quality, and the single most important safeguard of all: the pre-production physical sample.
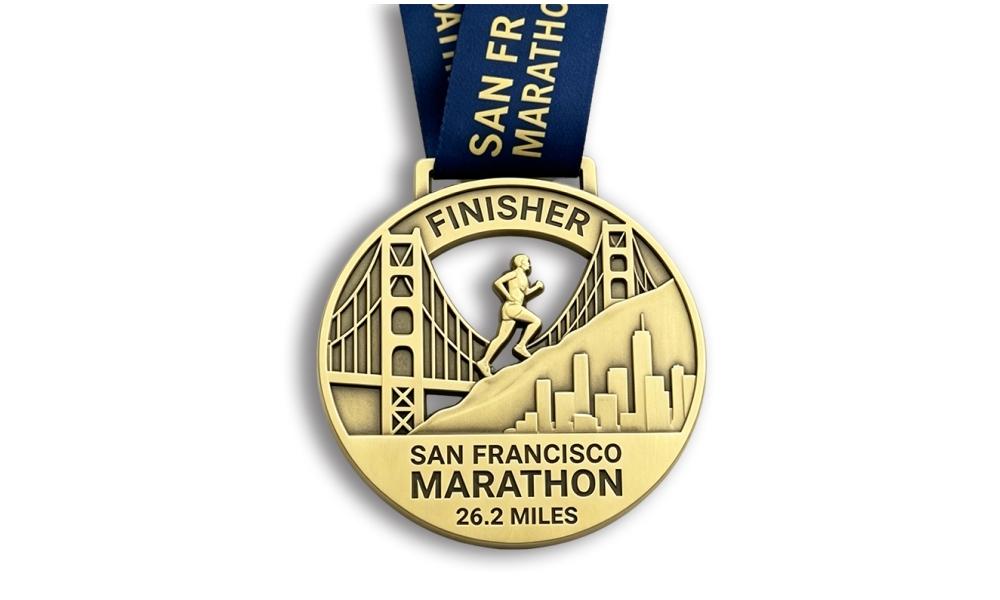
Here's a quick-reference checklist covering what to physically inspect when comparing samples from different custom medal manufacturer candidates.
| Inspection Area | What Good Looks Like | Warning Sign |
|---|---|---|
| Metal Weight | Solid, dense feel consistent with true zinc alloy | Suspiciously light or hollow-feeling for its size |
| Thickness | Matches quoted mm spec when measured with calipers | Noticeably thinner than quoted (e.g., 2.8mm vs. quoted 3.5mm) |
| Edge Polish | Smooth rim, no burrs or sharp corners | Rough edges, visible casting flash, sharp points |
| Plating Surface | Even, consistent shine or antique tone throughout | Scratches, pitting, bubbles, or dull/inconsistent patches |
| Enamel Color | Matches PMS/Pantone code accurately, clean fill lines | Off-shade color, bleeding into adjacent lines, thin fill |
| Ribbon | Smooth, soft polyester or satin; sharp printed graphics | Rough, frays easily; blurry or faded print |
| Stitching | Reinforced V-sew, holds firm under weight/tension | Single straight stitch line, loose or easily pulled |
The very first thing you notice when handling two medals side by side is often the most revealing: weight and density are difficult for a lower-quality supplier to fake, and they say a great deal about what's actually inside the casting.
Genuine, high-density zinc alloy has a distinctive, substantial heft that's hard to replicate with cheaper filler metals, tin-heavy blends, or medals cast with internal hollow sections to save material cost. When comparing samples from different suppliers, hold them side by side at the same nominal size — a noticeably lighter piece, even if it looks visually identical in photos, often signals a lower-density material substitution or hollow casting technique that won't hold detail or durability as well over time. This single hands-on comparison is one of the fastest ways to separate genuinely well-made samples from ones that only photograph well.
Don't rely on visual estimation alone — use a simple pair of digital calipers to measure a sample's actual thickness against the specification stated in your quotation. A supplier quoting a 3.5mm medal that actually delivers a 2.8mm sample has effectively reduced material cost without adjusting price accordingly, and that difference is immediately measurable, not a matter of opinion. This is a fast, objective, five-minute check that removes any ambiguity from a supplier's specification claims.
Plating quality determines both how a medal looks on day one and how well it holds up over months or years of handling — and it's an area where the difference between a skilled and an unskilled custom medal manufacturer becomes immediately visible under close inspection.
Run a finger gently along the medal's outer edge and any cutout details. A well-finished medal should feel smooth throughout, with no rough burrs, casting flash, or unexpectedly sharp corners — these are signs of a rushed or lower-quality finishing process, and beyond looking unpolished, sharp edges on a medal worn around the neck are a genuine practical annoyance and, in some cases, a minor safety concern for younger recipients.
Examine the plated surface closely under good lighting, turning the medal to catch reflections at multiple angles. Look specifically for tiny pits or bubbles in the plating (a sign of poor surface preparation before plating was applied), inconsistent shine across the surface (patches that are duller or shinier than the rest), and fine scratches that suggest careless handling during production or packing. Uniform, consistent plating across the entire surface — including inside recessed detail areas, which are harder to plate evenly — is a genuine marker of production care.
Quality plating typically includes a clear protective sealant layer over the metallic finish, specifically to resist oxidation from sweat, humidity, and general handling over the medal's lifespan. While this is harder to assess visually in a brand-new sample, it's worth asking the supplier directly what sealant process they use and whether they can share examples of medals from past orders that have been in circulation for a year or more, to get a sense of how the finish actually holds up in real-world conditions rather than just on delivery day.
Color accuracy and fill precision are where a supplier's attention to detail — or lack of it — becomes most obvious, since enamel work is inherently a hand-finished, quality-dependent process.
If your event has established brand colors with specific Pantone (PMS) codes, request that your sample be matched against those exact codes rather than an approximate visual match. Compare the physical sample directly against a printed Pantone swatch or your official brand guideline document under neutral lighting — enamel color that looks "close enough" on screen can read as noticeably off once compared to an actual color reference, and a supplier experienced in accurate PMS matching will typically get this right on the first sample rather than requiring several rounds of correction.
Inspect the boundaries between different enamel color sections closely. Good enamel work stays cleanly within its recessed cell, level with (or very slightly below) the surrounding raised metal lines; poor-quality work often shows color bleeding across a boundary line into an adjacent section, or enamel that's inconsistently filled — noticeably thinner and more recessed in some spots than others across the same medal. Both issues indicate rushed hand-filling and inadequate quality inspection before the piece left the factory.
If your design incorporates specialty effects — glitter enamel, fine 3D sculptural detail, or cutout sections — pay particular attention to consistency across the piece. Glitter enamel should be evenly distributed rather than clumped or sparse in patches; 3D sculptural elements should show crisp, well-defined edges rather than soft, muddy transitions that suggest the mold wasn't engineered with sufficient depth; cutout sections should have clean, precise edges without ragged or uneven punch-through. These specialty techniques are exactly where the gap between a skilled and an unskilled manufacturer becomes most visible, since they require both design expertise and precise production control to execute well.
Ribbon quality is frequently overlooked in supplier comparisons, yet it's a component recipients handle directly and repeatedly, making its quality highly visible in practice.
Feel the ribbon fabric directly — a quality ribbon should have a smooth, substantial, satin-like hand-feel rather than a thin, rough, or scratchy texture. Check the cut edges specifically for signs of fraying, since low-grade webbing tends to unravel at the edges relatively quickly with normal handling, while a properly finished ribbon edge stays clean and intact.
Examine any printed text or logos on the ribbon closely for edge sharpness and color vibrancy. Dye-sublimation printing, done well, produces crisp, high-resolution graphics with clean logo edges and vivid, saturated color; lower-quality screen printing can appear comparatively flat, slightly blurred at fine edges, or prone to fading and cracking after repeated folding or handling. This difference is usually obvious on close inspection even in a brand-new sample.
Test the stitching at the point where the ribbon loop closes and connects to the medal's hardware. Gently but firmly tug the ribbon loop to get a sense of how securely it's constructed — reinforced V-sew stitching, with multiple overlapping passes, should feel noticeably firmer and more resistant to give than a single straight seam. This is a particularly important check for heavier medals, since this exact junction is where cheaper ribbon assembly most commonly fails under real-world use.
Every inspection technique above depends on having an actual physical object to examine — which makes the sampling process itself the single most important step in evaluating any custom medal manufacturer.
It's worth distinguishing between two different kinds of samples, since both serve a purpose but neither substitutes for the other. An existing sample kit — a collection of a supplier's past work in various styles and finishes — is useful early on for gauging general skill level, material quality, and finishing consistency before you've even finalized your own design. A pre-production proof, by contrast, is a physical sample made specifically from your actual approved artwork, using your exact specified material, size, and plating — and this is the sample that genuinely matters before committing to a full production run. Never treat a supplier's general capability samples as sufficient confirmation of what your own specific order will look like; always insist on a true pre-production sample of your own design before authorizing mass casting.
Zinc alloy castings typically have a distinctive heavy, dense feel relative to their size, and support fine 3D relief detail with clean, sharp edges. Iron medals, produced through die-struck stamping rather than casting, are generally limited to flatter, simpler 2D designs and often feel comparatively lighter for the same visual size, though this can be harder to judge by feel alone. The most reliable way to confirm the base material is to ask the supplier directly and request written material confirmation in your quotation and order documentation — a reputable manufacturer will state this clearly and without hesitation.
Yes, without exception, for an order of this size. The relatively small cost (or, with many manufacturers, no cost, or a cost credited against your final order) of a pre-production sample is negligible compared to the risk of discovering a color, weight, or finish problem only after 1,000 pieces have already been cast. A supplier confident in their work will readily provide this sample and often waive or credit its cost once you proceed to the full order; reluctance to provide a genuine pre-production sample before a large commitment is itself a significant warning sign.
Look specifically for a written guarantee that bulk production will match your approved pre-production sample, along with a clearly defined remedy if it doesn't — reproduction of the defective batch, a partial credit, or a full refund. Vague verbal assurances or a "case-by-case" answer when you ask this question directly should be treated with caution; a manufacturer confident in their own quality control process will typically have this guarantee documented and will state it clearly and consistently when asked.
Every inspection point in this guide is something you can verify directly with Shenzhen Vistarts Craft Co., Ltd. before committing to production. We are a self-owned factory established in 2011, with over 10,000 square meters of production space, 150+ employees, 50+ modern machines, and 20+ professional engineers, giving us direct, in-house control over material selection, plating, enamel work, and ribbon assembly at every stage.
Our dedicated 10+ person QC team inspects raw materials, in-process production, and finished goods for exactly the issues covered in this guide — proper zinc alloy density and thickness, clean plating uniformity, accurate PMS color matching, and reinforced V-sew ribbon stitching — backed by ISO9001 certification, RoHS and CE compliant materials, and factory audit approval from Disney and Universal Studios. We provide free 2D/3D digital artwork proofs plus true pre-production physical samples made from your exact approved design, so you can put every technique in this guide to the test before authorizing mass production, backed by a full refund guarantee if bulk production ever deviates from your approved sample.
Want to see and feel the quality difference for yourself? Request a pre-production sample for your next design from our sales team — with 3+ years of dedicated order-follow-up experience — and inspect it against every checkpoint in this guide. Visit vistarts.com to get started today.
58 South Union Road, South Union Community, Shenzhen, Guangdong, China